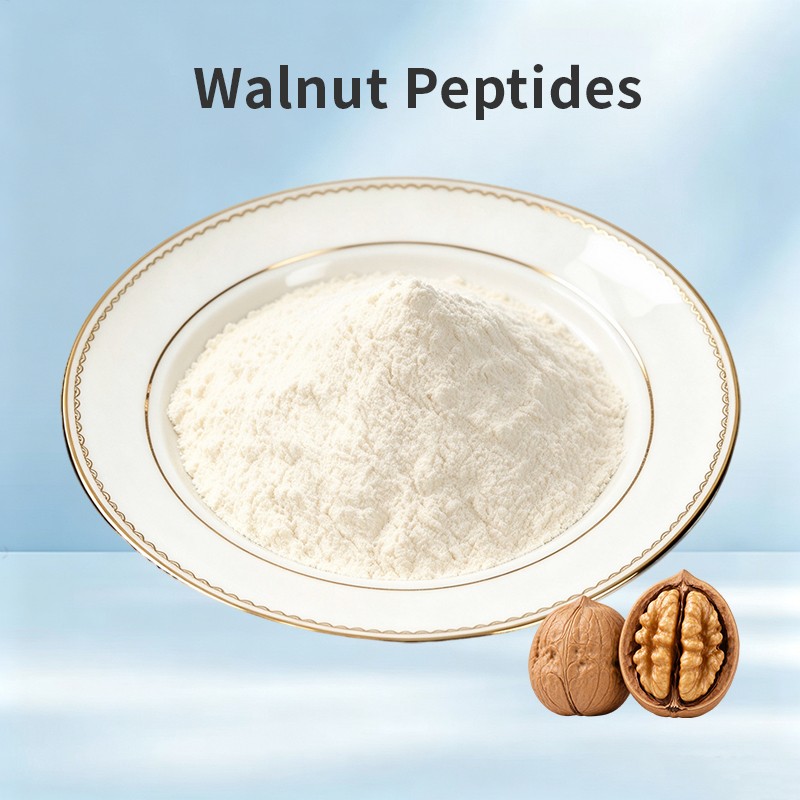
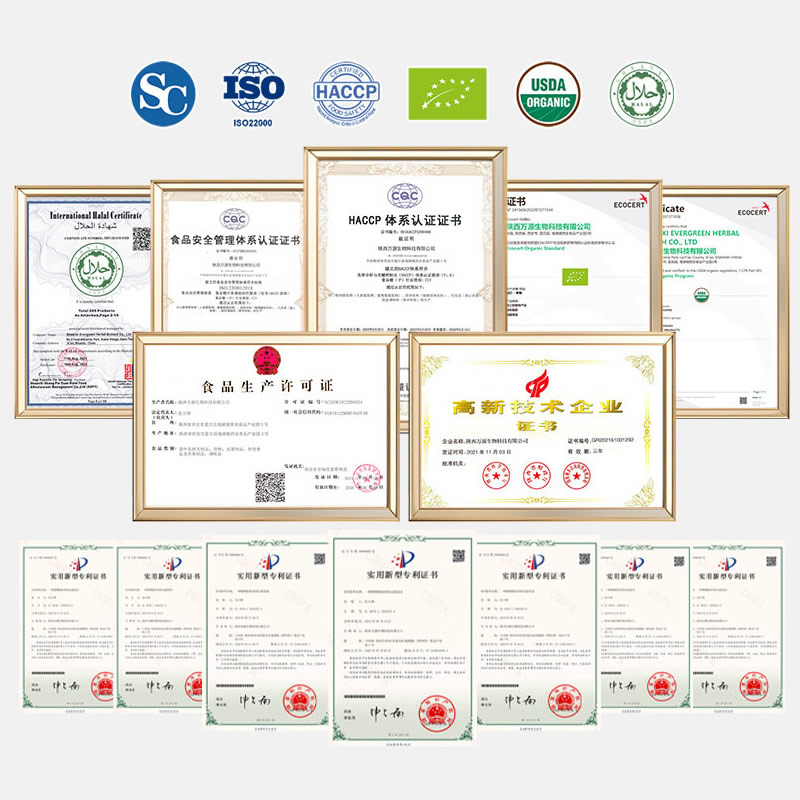
We supply food-grade walnut peptides with standard molecular weight range. Custom specifications can be tailored to fit different food processing, beverage blending and formula development requirements. Each batch is tested and verified by third-party authoritative laboratories to comply with international food safety and clean-label production standards.
Raw Material Source: Walnut kernel protein
Processing Technology: Raw material sorting, walnut protein separation, directional enzymatic hydrolysis, membrane purification, concentration, spray drying, sterile screening
Appearance: Uniform light beige fine powder, subtle natural nutty scent, no peculiar smell, no mildew or deterioration
Main Components: Short-chain walnut oligopeptides, amino acids
Molecular Weight: Mainly below 1000 Da, customizable range available
Solubility: Good water solubility, dissolves easily in water to form translucent liquid
Key Features: Walnut-derived peptide source, low impurity content, stable batch performance, favorable solubility, clean formula, gentle nutty flavour
Available Certifications: ISO22000, Halal, Kosher, Non-GMO compliant
Shelf Life: 24 months under sealed, cool, dry and dark storage conditions
Raw Material Natural Characteristics
Walnut is a widely recognised nut crop containing abundant plant protein. Our walnut peptides are produced through enzymatic breakdown of walnut protein, converting macromolecular protein into short peptide segments. The product delivers good solubility and easy mixing within various formula systems, aligning with the global development trend of plant-based and clean-label food ingredients.
Nut Protein Origin: Made from walnut kernel protein, nut-derived peptide raw material without mixing protein sources from other species.
Directional Enzymatic Hydrolysis: Adopt targeted enzymatic treatment to split walnut protein into small peptide segments, sustaining consistent molecular weight distribution from batch to batch.
Stable Sensory Consistency: Unified production standards ensure consistent colour, aroma and solubility across different batches, improving the sensory and application performance of finished compound products.
Wide Formula Adaptability: Fine powder texture supports uniform mixing, compatible with various solid and liquid food formula systems for diversified applications.
Disclaimer: This product is a food-grade plant peptide raw material for formula compounding only. All descriptions are limited to raw material natural attributes and application characteristics, excluding medical judgment, treatment and health intervention claims.
Application Fields
With nut-derived peptide attributes, stable batch quality and excellent solubility, walnut peptides are widely applied in global functional food, beverage and nutritional product manufacturing industries:
Nutritional Meal Replacement Foods: Nut-grain composite meal powder, food nutritional fortification ingredients, plant protein compound formula materials
Functional Beverage Formulas: Solid drinks, peptide beverage bases, nut flavoured beverage compound raw materials
Bakery & Snack Products: Nutritional additives for baking foods, nut snacks and filling blending ingredients
Dietary Blend Formulas: Composite nutritional powder, plant peptide formula components
Clean-Label Food R&D: Standard plant peptide raw material for plant-based and clean-label new product development
Our Supplier Advantages
We adopt standardized walnut raw material screening and directional enzymatic hydrolysis production lines. Strict raw material source control and complete batch inspection mechanisms ensure stable solubility, pure nutty flavour and consistent composition for bulk export orders.
High-Quality Raw Material Selection: Select qualified walnut protein raw materials, strictly remove impurities and foreign substances to stabilize raw material quality foundation.
Directional Enzymatic Hydrolysis Process: Use gentle targeted enzymatic hydrolysis technology to obtain target peptide segments, maintaining stable molecular weight distribution.
Multi-Stage Membrane Purification: Multiple membrane filtration procedures remove macromolecular protein and tiny impurities, helping achieve stable solubility.
Full Batch Quality Control: Each batch undergoes appearance, moisture, molecular weight, heavy metal and microbial testing before shipment, meeting international food-grade export standards.
Flexible Custom Service: Support specification and packaging customization, providing complete export documents including COA and MSDS.
Packaging & Storage Guidelines
Standard Export Packaging: 1kg aluminum foil vacuum bag; 25kg food-grade fiber drum with inner plastic lining bag
Storage Conditions: Store in cool, dry, dark and ventilated warehouse, avoid high temperature, humid environment and direct sunlight exposure.
Storage Reminder: Walnut peptides are sensitive to moisture. Please keep tightly sealed after opening to prevent moisture absorption, caking and changes to product properties.
FAQ
Q1: What is the source of your walnut peptides?
A1: Our walnut peptides are derived from walnut kernel protein, produced via enzymatic hydrolysis and purification, with no other protein sources blended.
Q2: Does this product contain added sugar or artificial additives?
A2: Bulk walnut peptides are produced with directional enzymatic hydrolysis and purification. No added sugar, artificial pigments, flavours, preservatives or inert fillers are added, suitable for clean-label product production.
Q3: What are MOQ and delivery time?
A3: Small sample orders are supported for quality testing and formula trial. Conventional specifications are in stock for fast delivery, and customized requirements can be confirmed separately.